Particle Contamination Monitoring for Gigafactories
Layered particle monitoring for battery-cell production—from HVAC supply air and cleanrooms to equipment and critical process locations.
Related products
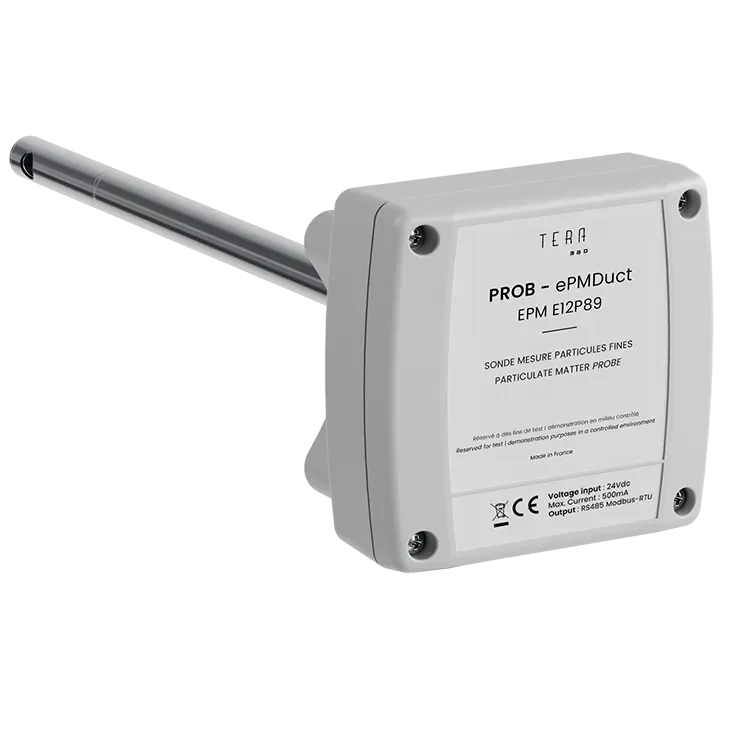
PMDuct
Monitor changing particle conditions inside air-handling and supply-duct systems before air reaches clean and dry production areas.
Explore PMDuct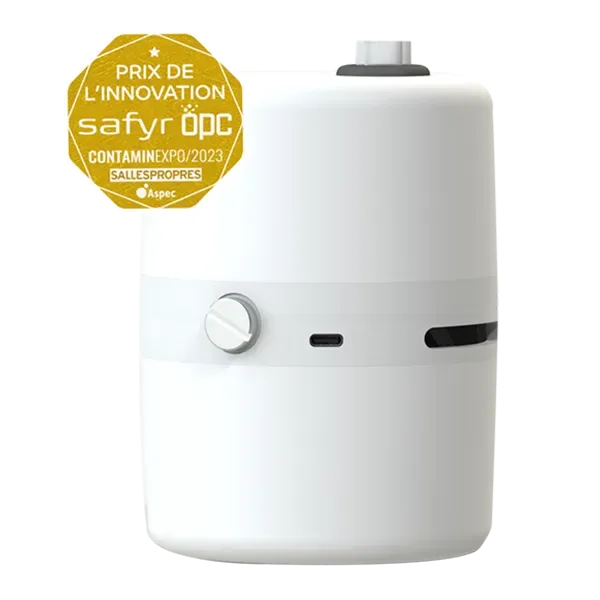
SafyrOPC Instrument
Continuous ISO 21501-4-calibrated particle counting at selected cleanroom and controlled-area locations.
Explore SafyrOPC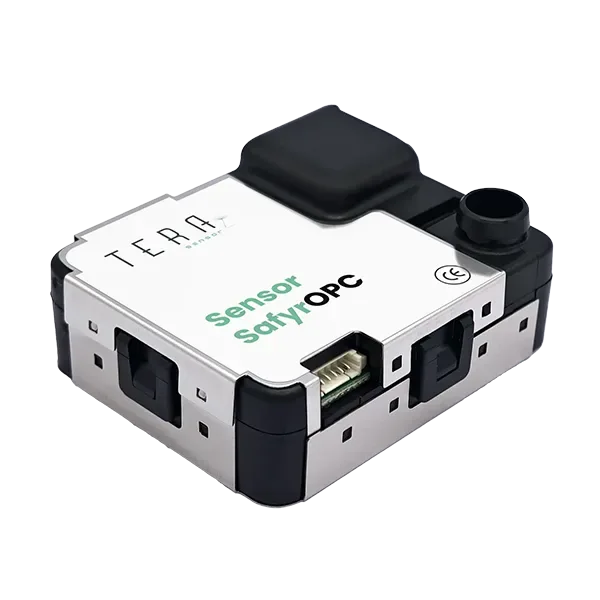
Sensor SafyrOPC
Compact OEM optical particle counter module for integration into battery-production equipment, clean and dry-room monitoring systems and critical process locations. Each module is individually calibrated according to ISO 21501-4 and supplied with a unit-specific calibration certificate.
Explore Sensor SafyrOPC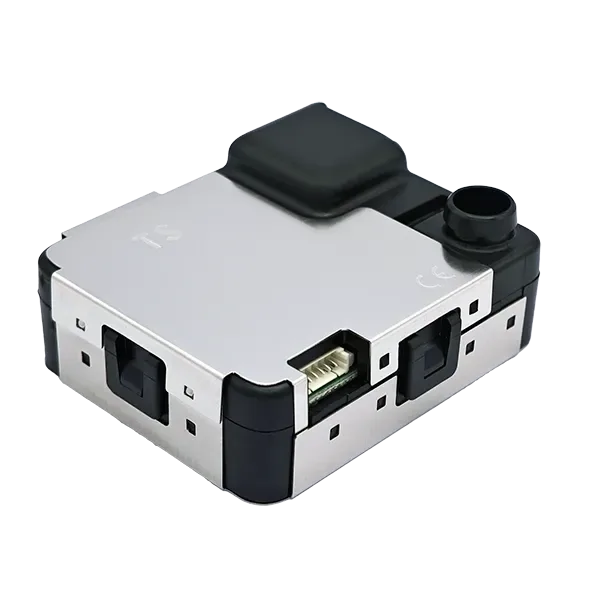
NextPM
Cost-effective PM monitoring for adjacent environments, technical areas and locations that do not require cleanroom-classification data.
Explore NextPM
High-throughput battery production leaves little room for undetected contamination
Battery-cell manufacturing operates at high throughput while requiring tight control of materials, geometry, moisture and technical cleanliness. Foreign particles can originate from raw materials, equipment wear, electrode cutting, material handling, maintenance or the surrounding production environment.
Some contamination defects are only identified during formation, end-of-line testing or later failure analysis. By then, the potentially affected production window may include a significant number of cells, making containment and root-cause investigation more difficult.
This challenge is especially important during gigafactory ramp-up. Fraunhofer FFB and RWTH Aachen report that overall scrap rates of 15–30% are common during the first years of battery-cell production, with rates still around 10% after five years. These figures cover all causes of production scrap and must not be attributed solely to particle contamination.
Source: Fraunhofer FFB and PEM RWTH Aachen, "Mastering Ramp-up of Battery Production", 2024.
Small deviations become high-volume losses
At gigafactory throughput, the time between a contamination event and its detection can substantially increase the number of potentially affected cells.
Some defects remain latent
Foreign-matter contamination may only become visible during formation, electrical screening or subsequent failure analysis.
The source is difficult to localize
HVAC systems, materials, operators and multiple production machines can all contribute to the particle conditions observed near the process.
Monitoring coverage remains constrained
Using high-cost cleanroom counters at every possible location makes broad and simultaneous coverage difficult to justify.
Why particle monitoring in battery-cell production requires a layered approach
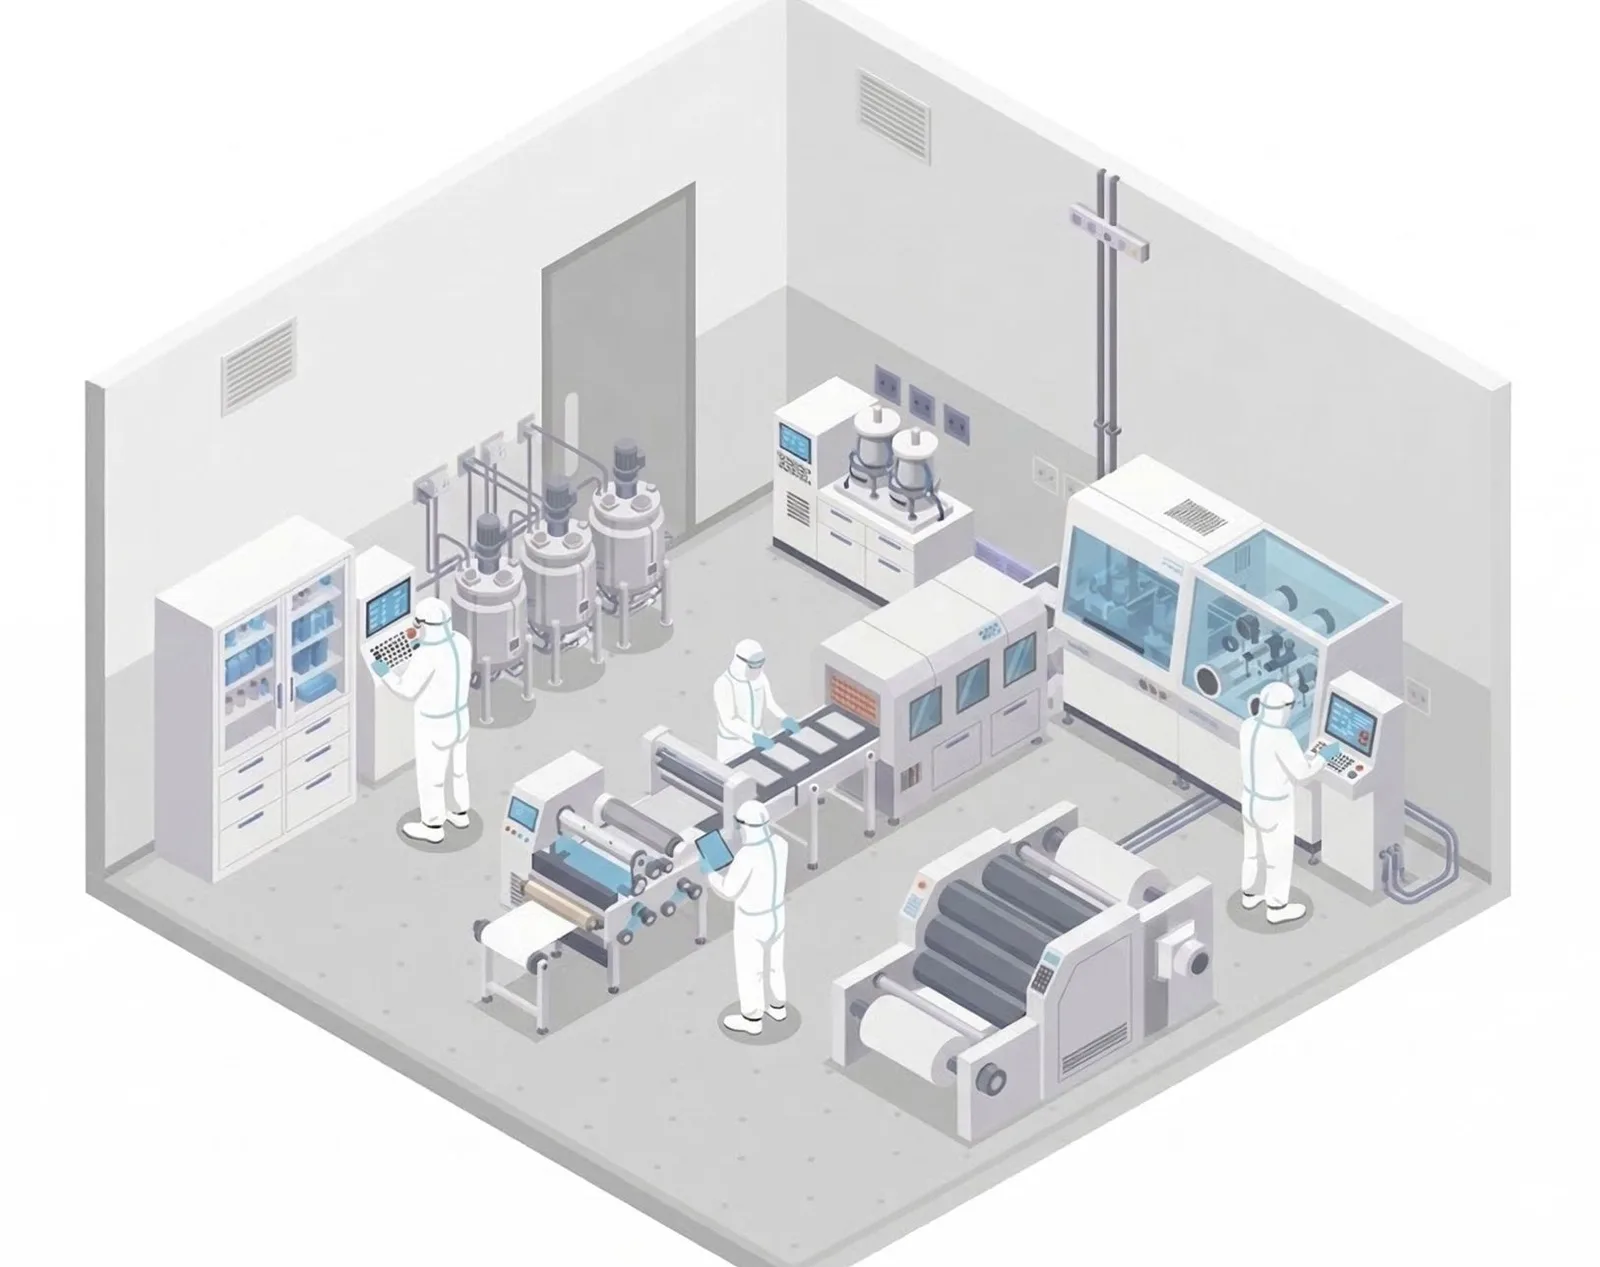
Gigafactories combine clean and dry rooms, high-speed electrode processes, enclosed equipment and large HVAC infrastructures. A single instrument and a single measurement principle cannot provide the most useful information at every location.
Multiple particle sources
Electrode materials, metallic wear, cutting operations, fibers, maintenance and material handling can generate particles with different sizes and properties.
Short and localized events
Transient emissions during slitting, stacking, machine interventions or material transfers may not be captured by periodic or distant measurements.
Large and segmented production areas
Air-handling units, dry rooms, clean zones, airlocks and individual machines create numerous potential contamination paths.
Different metrological requirements
Peripheral and HVAC trending can use PM measurements, while cleanroom and critical-process locations require calibrated particle counting in number concentration.
Sequential monitoring creates blind periods
A centralized manifold measures locations one after another, potentially missing short excursions while another point is being sampled.
Airborne monitoring has defined limits
Optical monitoring detects changes in concentration and size distribution but does not identify chemical composition or prove that a particle entered a cell.
Effective monitoring requires the right combination of measurement technology, sampling location and production context.
SOLUTION ARCHITECTURE
Layered particle monitoring from air supply to cell assembly
Relying on a few high-cost particle counters limits simultaneous coverage across a large battery factory. TERA Sensor combines complementary monitoring technologies so that each point uses the measurement principle best suited to its location and purpose.
The objective is to detect changing particle conditions as early as possible, follow their propagation and maintain ISO 21501-4-calibrated counting close to critical cleanroom and process locations.
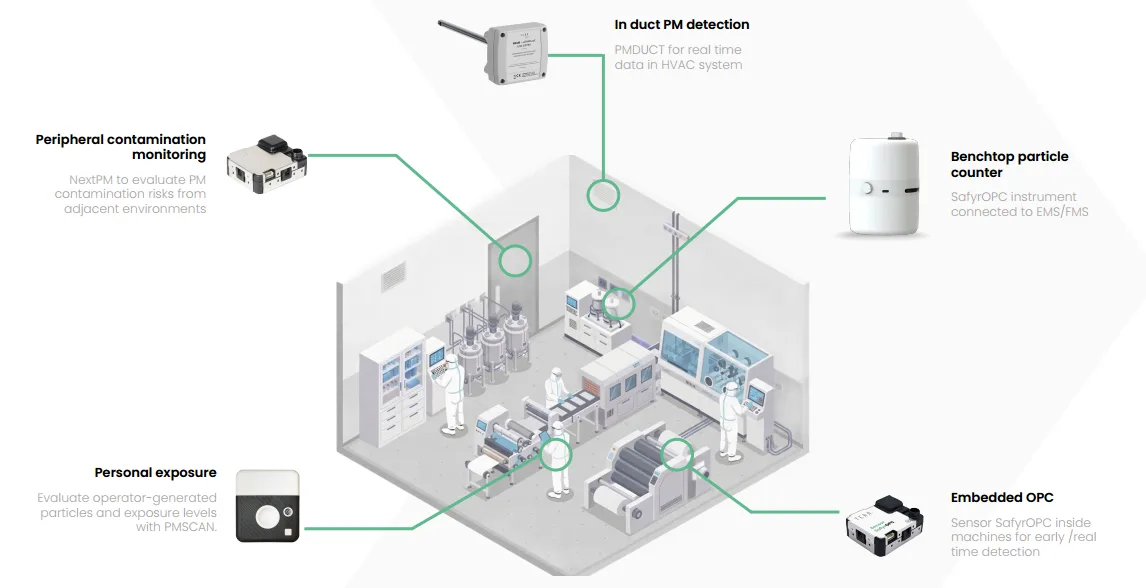
HVAC and supply-air monitoring
Detect changing particle conditions before air reaches clean and dry production areas.
Distributed cleanroom monitoring
Extend simultaneous ISO 21501-4-calibrated particle-count coverage across selected production locations.
Embedded equipment monitoring
Integrate calibrated particle counting closer to critical machines and production operations — electrode cutting, stacking or winding, cell assembly.
Peripheral particle monitoring
Monitor particle trends in adjacent environments, technical areas and logistics interfaces such as airlocks and material transfer.
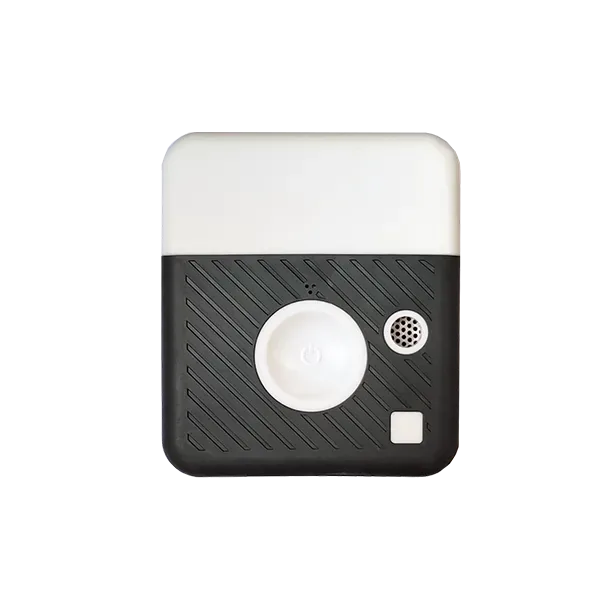
Mobile process investigation
Investigate transient events related to operators, maintenance, material handling or specific operations.
Earlier detection
Monitor abnormal conditions upstream and around production before they reach the most critical process location.
The right data at each point
Use PM trending where relative changes are needed and calibrated particle counting where cleanroom metrology is required.
Denser coverage
Increase the number of relevant monitoring points without using the most expensive architecture everywhere.
Faster source localization
Compare HVAC, room and equipment data to identify where an abnormal particle event first appeared.
One measurement technology does not need to cover every risk. By combining complementary sensors across the production path, TERA Sensor helps collect the right particle information at the point where it is most useful.
Complementary particle-monitoring solutions for battery-cell production
Specifications, communication and calibration for each monitoring technology in the architecture above.
PMDuct
In-duct monitoring for detecting changing particle conditions in the HVAC supply path before air enters clean and dry production areas.
- Direct in-duct installation
- Integrated pump
- PM₁, PM₂.₅ and PM₁₀
- Up to 10,000 µg/m³
- Temperature and relative humidity
- Modbus RS485 RTU
SafyrOPC Instrument
Compact standalone monitoring point designed to extend ISO 21501-4-calibrated particle coverage across cleanrooms and controlled areas.
- SafyrOPC calibrated sensing module
- Wired or battery operation
- Wireless communication options
- Wall-mounting capability
- Replaceable calibrated sensor
- Reduced calibration downtime
Sensor SafyrOPC
OEM particle counter module for embedded monitoring in battery-production machines, isolators and local contamination-monitoring systems. Suitable for integrators developing equipment-level particle monitoring around electrode cutting, stacking, winding, cell assembly and other contamination-sensitive process steps. For equipment manufacturers and system integrators, Sensor SafyrOPC provides an OEM particle-counting core that can be embedded directly into production equipment and local monitoring architectures.
- Individual ISO 21501-4 calibration certificate
- Five cumulative particle channels, 0.3 to 10 µm
- 2.83 L/min sampling flow
- UART and Modbus communication
- Compact 62 × 52 × 23 mm format
- Filtered exhaust
NextPM
Cost-effective PM monitoring for adjacent environments, technical areas and locations that do not require cleanroom-classification data.
- PM₁, PM₂.₅ and PM₁₀ in real time
- Five particle-size bins, 0.3 to 10 µm
- Patented humidity management
- AQ-SPEC validated performance
- UART and Modbus communication
- Not intended for ISO 21501-4 cleanroom classification
Need to investigate a transient production event?
PMScan provides a mobile particle-data point for investigating operator movements, maintenance, material transfers or specific production operations.
PMDuct and NextPM report PM trend data. SafyrOPC Instrument and Sensor SafyrOPC provide ISO 21501-4-calibrated particle counting. No single product on this page determines cleanroom classification, compliance or production scrap on its own.
From late defect detection to earlier production insight
Distributed particle monitoring adds time and location context to battery-production data. It helps teams detect abnormal particle conditions, define the potentially affected production window and investigate whether the event originated in the HVAC system, production area, equipment or operation.
Detect transient production events
Capture short particle changes associated with equipment, interventions, material transfers or specific production phases.
Reduce the affected production window
Use precise timestamps to identify which production period requires investigation instead of treating a longer period as potentially affected.
Accelerate root-cause analysis
Compare particle data from HVAC, cleanroom and equipment locations to determine where an event first appeared.
Support ramp-up and yield improvement
Add environmental and process-context data to the investigation of recurring defects and unstable production conditions.
Increase monitoring density
Add relevant points across large production areas without using a high-cost cleanroom counter at every location.
Verify corrective actions
Compare conditions before and after cleaning, maintenance, filtration, sealing or process changes.
Strengthen production traceability
Correlate particle events with line, equipment, shift, maintenance and batch or lot timestamps.
Designing a particle-monitoring architecture for battery-cell production?
Effective monitoring depends on more than sensor selection. Production layout, HVAC architecture, sampling location, process speed, data synchronization, communication, calibration strategy and maintenance all influence the value of the final data.
TERA Sensor supports monitoring architecture, sensor selection, sampling design, equipment integration and calibration strategy. TERA Tronics can support electronics, connectivity, prototyping, industrialization and series manufacturing.
For equipment manufacturers and system integrators, TERA Sensor provides direct engineering support from sensor selection and sampling architecture through electronics, firmware, prototype validation and industrialization. Sensor SafyrOPC is designed, calibrated and manufactured in France.
- TERA Sensor: particle measurement, sensor selection, sampling architecture, integration and calibration.
- TERA Tronics: electronics, prototyping, industrialization and series manufacturing.
FAQ
Foreign particles introduced during electrode processing, cutting, stacking or assembly can affect cell quality and consistency. Some contamination-related defects are only identified during formation, end-of-line testing or later failure analysis, by which point the potentially affected production window may include a significant number of cells — making containment and root-cause investigation more difficult.
Electrode materials, metallic wear, slitting and cutting operations, fibers from separators or packaging, maintenance interventions and material handling can all generate particles. HVAC systems, operators and multiple production machines can also contribute to the particle conditions observed near the process.
Distributed particle monitoring adds time and location context that can help teams narrow the potentially affected production window and accelerate root-cause investigation, which can support scrap-reduction efforts. It does not by itself reduce scrap: reported ramp-up scrap rates (15-30% in the first years, still around 10% after five years, per Fraunhofer FFB and RWTH Aachen) cover all causes of production scrap, not particle contamination alone.
No. Airborne particle monitoring detects concentration changes and helps localize where they occur, but it does not identify particle chemistry, prove that a particle entered a cell, or replace inline electrode inspection, separator testing, formation screening, computed tomography or end-of-line electrical testing. It is one layer of a broader quality-control strategy.
PM monitoring (NextPM, PMDuct) reports mass-concentration trends — useful for peripheral areas, technical rooms and HVAC supply air, where a relative change matters more than a calibrated count. ISO 21501-4-calibrated particle counting (SafyrOPC Instrument, Sensor SafyrOPC) provides traceable number concentration, required for cleanroom and critical-process locations.
PMDuct is installed in the HVAC supply-air path, upstream of clean and dry production areas, to detect changing particle conditions in the air-handling system before that air reaches the process. It measures PM mass fractions and complements room-level counters — it is not a substitute for ISO 21501-4 particle counting inside the cleanroom.
At selected cleanroom, dry-room or controlled-area locations where continuous, calibrated particle-count coverage is required — chosen according to airflow patterns, critical operations and equipment interfaces, as with any cleanroom monitoring plan.
A single high-cost particle counter, or a manifold sampling several locations sequentially, limits simultaneous coverage and can miss short excursions while sampling another point. A distributed architecture — several lower-cost monitoring points, each measuring continuously — increases the number of locations that can be watched at the same time.
SafyrOPC provides ISO 21501-4-calibrated particle-count data that can support cleanroom classification and monitoring strategies, subject to the applicable sampling plan and validation requirements. It samples at 2.83 L/min and is positioned for ISO 5-8 and GMP Grades B-D contexts, not as a Grade-A-equivalent primary counter.
Yes. Sensor SafyrOPC communicates over UART and Modbus, PMDuct and NextPM over Modbus RS485, and the SafyrOPC instrument offers wired and wireless options — so monitoring points can feed the facility data architecture alongside the parameters already collected.
Particle data can be timestamped and compared against line, equipment, shift, maintenance and batch or lot records to support traceability and investigation. Setting up that correlation depends on the facility data architecture and is not automatic from the sensor alone.
Optical particle counting and PM sensing are not inherently limited by the low humidity of a dry room; operating range and any environmental limits are documented in each product datasheet and should be checked against the specific dry-room conditions before deployment.